Samudy Jingchuang Injection Molding (Shenzhen) Co Ltd Yu Ling
Introduction:
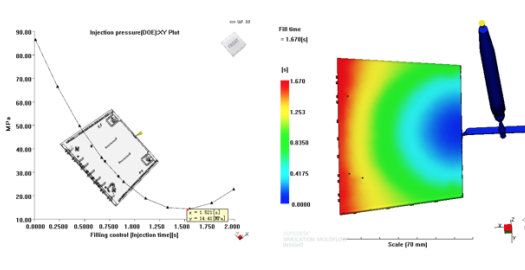
Moldflow software was used to analyze the average volumetric shrinkage of the product and simulate the injection molding process of 3C product appearance parts. Through the analysis of injection flow, the optimal gate location of the part was determined, and defect locations such as air traps and weld lines were predicted and displayed. Combined with changes in injection pressure and clamping force, the filling process, temperature variations, and molded part quality analysis, this helped process engineers identify the causes of defects before mold trials, thereby improving mold structure design and product structure to increase the success rate of mold trials.
Case Description:
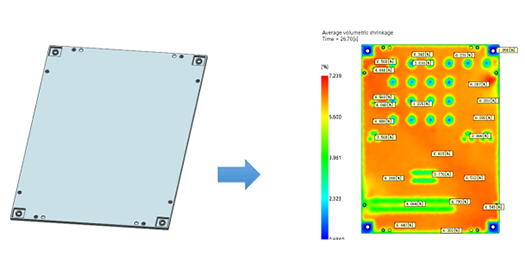
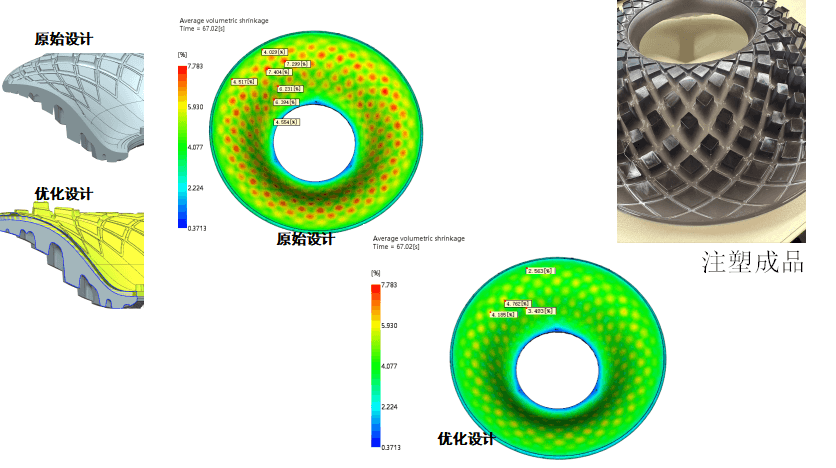
As shown in Figure 1, the product is a speaker component, single-color molding, made of PC material
The left image is the 3D drawing; the right image shows the shrinkage problem points identified by MF analysis
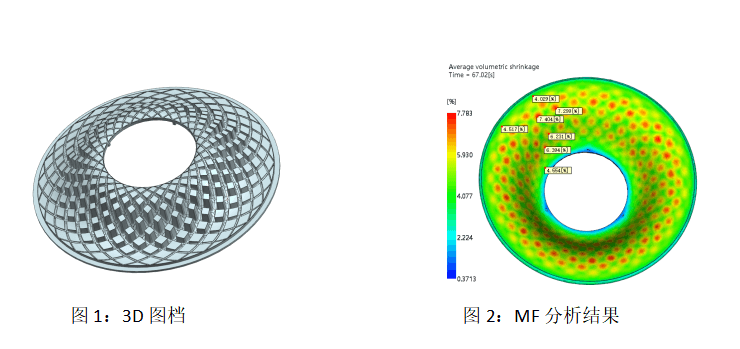
The shrinkage occurred on the appearance surface, causing a serious appearance defect!
In this case, the severity of the shrinkage was a defect that could not be predicted by experience alone. If the gate location and plan were adjusted only after mold trials, it would lead to increased mold development costs
Is it due to the product structure?
Because the customer's product structure is fixed and the appearance ID cannot be changed
Cause Analysis of Product Shrinkage:
We analyzed many types of gate designs, but none could improve the product shrinkage problem.
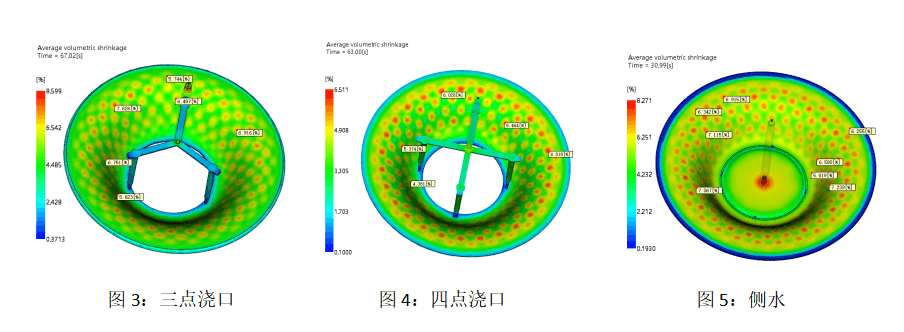
1. Improvement Plan:
Finally, we proposed converting the existing single-color product to two-color molding without changing the customer's ID
In the end, through MF verification and comparison, the problem was nipped in the bud
The final product met the customer's requirements.
Case Description:
Product Introduction: game console cover, single-color molding, PC material
The left image is the 3D drawing; the right image shows the shrinkage problem points identified by MF analysis
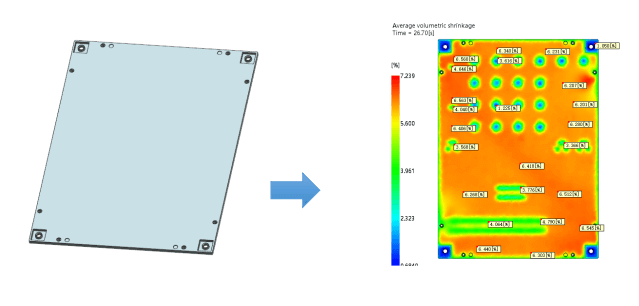
Shrinkage and stress marks appeared on the appearance surface, causing a serious appearance defect!
In this case, MF analysis enabled early prediction of shrinkage and product modification. With stress marks verified in advance, the mold modification cycle and the number of mold trials were reduced
Is it due to the product structure?
Because the customer's product structure is fixed and the appearance requirements cannot be changed
Cause Analysis of Product Shrinkage:
Looking at the current product, the main wall thickness is 3.2 mm while the local wall thickness is only 1.2 mm. Visually, there is definitely a risk of stress marks on the appearance
Finally, we proposed converting the existing single-color product to two-color molding without changing the customer's ID, and carried out MF verification
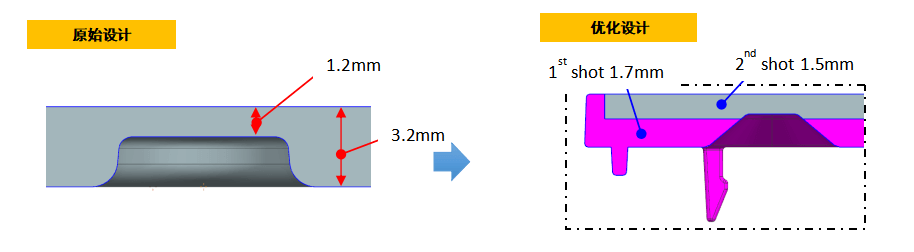
2. Improvement Plan:
Two-color verification 1: shrinkage was improved, but the analysis result still showed stress marks, and the actual product also had them
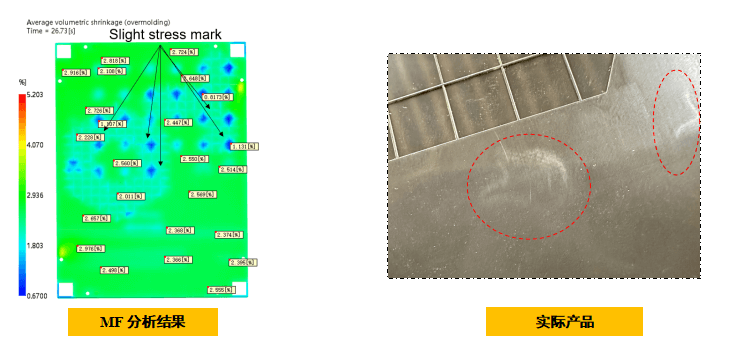
Verification 2: because this problem had been predicted in advance, we communicated with the customer immediately and added material locally to the first shot. Consistent with the MF analysis result, the appearance problem was resolved
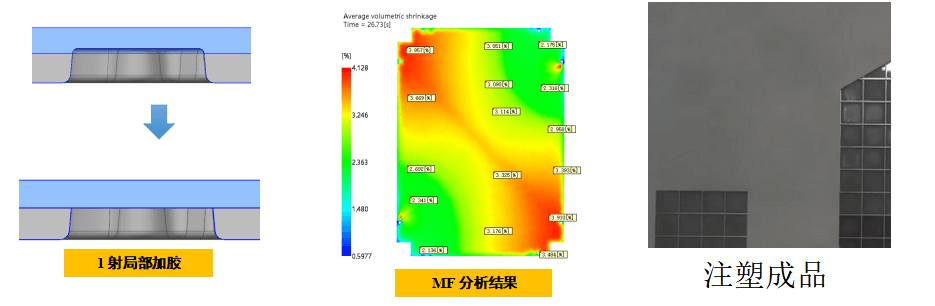
These products played a key role in the project. Through early MF analysis, we kept costs to a minimum
Predicting product defects in advance saved an average of CNY 100,000 in mold repair costs per mold
Predicting product defects in advance saved 3 mold trials, saving about CNY 20,000
With 20 similar molds per year, the total benefit was 20 x (10+2) = CNY 2.4 million
Using Moldflow
Shrinkage cause analysis before mold manufacturing — improvements made before mold opening
Improvement cost: 0 to tens of thousands (including quality upgrades)
Improvement time: 0 to a few days (same as above)
Quality Improvement
Conclusion:
Experience sharing: through the above two cases, we concluded that shrinkage and stress marks can be assessed through average volumetric shrinkage. If the result is less than 2%, the product will not show problems
Summarizing the two cases above, we need to combine actual products with the analysis data provided by Moldflow to give our professional recommendations and predict shrinkage and appearance stress risks in advance.
In Case 2, the product was changed from single-color to two-color molding, which solved the shrinkage problem. Although the groove of the second shot is very shallow, stress marks still occurred, and the actual mold trial product also had stress marks. Through verification by adding material to the first shot, for such two-color products, the second shot must have no recessed step at all to avoid stress marks.
Customer Testimonial
All products are required to be lightweight. Lightweighting is good for the environment and helps customers save costs. But it must be achieved without compromising quality, which is a challenge for the industry. How to make products as lightweight as possible while ensuring product quality has always been our goal. Moldflow software will play a major role in this.


 Business Scope
 Component Solutions